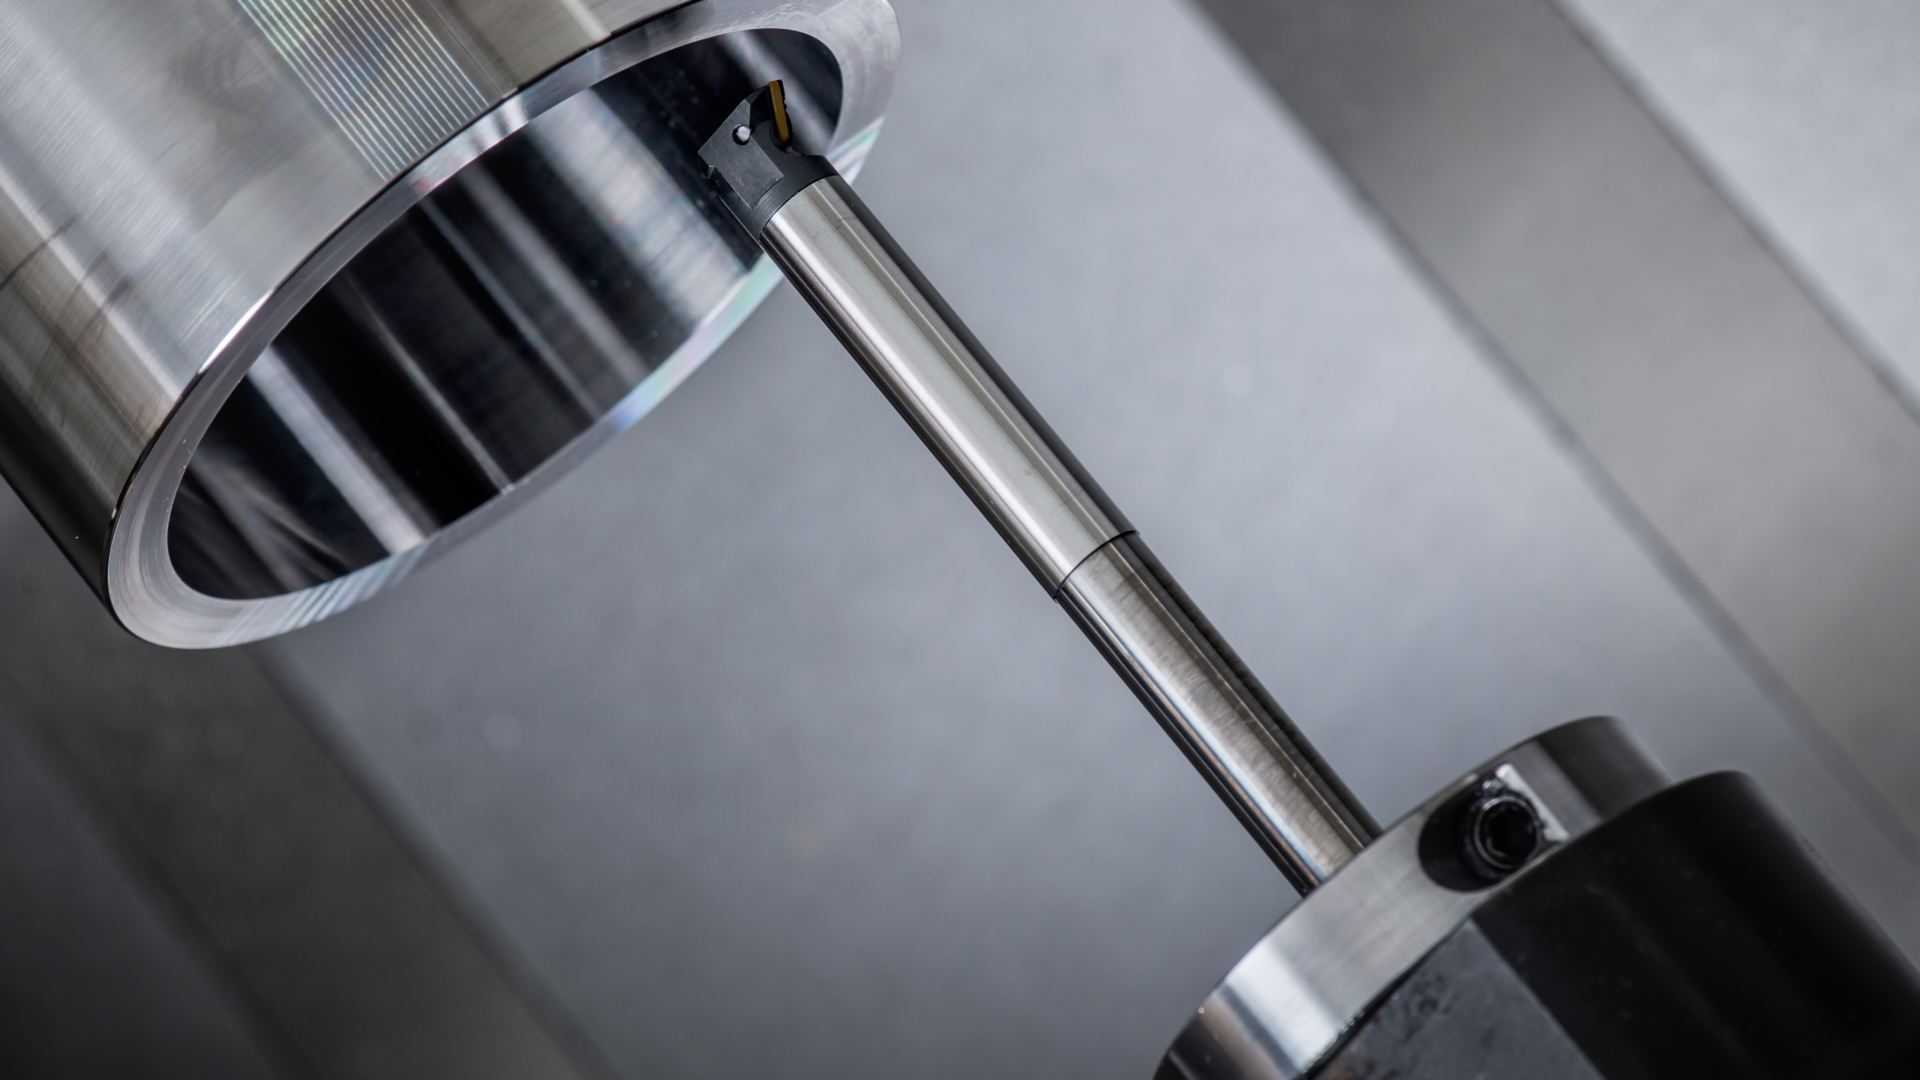
In metalworking, face milling serves as a broad umbrella term for generating flat surfaces. For basic, shallow surface machining, operators typically rely on very short, sturdy setups where rigidity is easily maintained. However, modern CNC manufacturing frequently requires machining features deep within workpieces, along tall vertical walls, or inside enclosed cavities.
When milling operations require an extended reach, standard rigid tool assemblies quickly hit their physical limits. Operations like shoulder milling, profile milling, and pocket milling demand long-reach configurations where radial forces and harmonic resonance excite chatter.
In these challenging scenarios, utilizing damped milling tools becomes essential to maintaining precision, tool life, and high metal removal rates. Investing in high-quality damped milling tools ensures that your shop can tackle complex, deep features without compromising on cutting speed.
Why Standard Setups Fail and Damped Milling Tools Succeed
Standard broad face milling with a low overhang allows the machine spindle to absorb cutting forces directly. However, as tool extension increases to reach deep features, rigidity drops drastically.
- The Cantilever Effect: Extended holders act as cantilevered beams. Dynamic deflection increases exponentially with overhang length (L/D ratio), making damped milling tools necessary to counteract bending motions and maintain dimensional accuracy.
- High Radial Force Displacements: Unlike basic face milling, which primarily directs forces axially into the spindle, shoulder, profile, and pocket milling generate substantial radial forces. Damped milling tools absorb the sideways push that would otherwise cause severe deflection and vibration.
- Harmonic Resonance: Periodic insert entries trigger continuous mechanical shocks. When these impacts match the reduced natural frequency of an extended holder, harmonic resonance develops rapidly, ruining surface finish (Ra) and micro-chipping carbide insert edges.
To overcome chatter on long-reach cuts without backing off on cutting parameters, shop floors rely on damped milling tools specifically designed for these demanding applications.
High-Reach Operations Demanding Damped Milling Tools
1. Shoulder Milling
Shoulder milling generates two perpendicular surfaces simultaneously using 90-degree square shoulder cutters.
- Force Distribution: Because cutting forces are directed almost entirely radially against the tool body, shoulder milling creates significant bending moments (direction where the tooling structure has the least rigidity) on extended holders.
- The Solution: Machining deep shoulders forces operators to extend tool length. Without vibration control, radial cutting force causes tool push-off, poor wall straightness, step-over marks, and rapid insert wear along with risks of tool chatter. Integrating damped milling tools into your setup eliminates these dimensional inaccuracies.
2. Profile Milling
Profile milling involves machining complex 2D and 3D contours, outer wall faces, and structural geometries.
- Dynamic Engagement: As the cutter follows multi-axis toolpaths, radial engagement and chip loads fluctuate continuously across angled and curved surfaces.
- The Solution: Extending a cutter to profile deep external walls introduces unstable harmonic vibration. These force variations trigger chatter marks across critical structural surfaces, which is why damped milling tools are critical for maintaining a smooth finish on complex profiles.
3. Pocket Milling
Pocket milling removes material inside enclosed boundaries to produce deep internal cavities, pockets, and aerospace structural frames.
- Interrupted & Cornering Loads: Pockets require helical entry or ramping, followed by tight cornering where radial cutter engagement spikes dramatically.
- The Solution: Enclosed pocket geometries mandate long tool overhangs. The combination of dynamic cornering loads and extended length generates intense vibration. This forces operators without damped milling tools to dramatically reduce feed rates and depth of cut. By utilizing damped milling tools, operators can maintain high metal removal rates even deep inside pockets.
Eliminating Chatter with MAQ Damped Milling Tools
While standard short and sturdy holders suit basic flat face milling, deep shoulder, profile, and pocket milling require active vibration suppression. Traditional tuned mass dampers require manual adjustment or complex formulas to match a single frequency – a process that fails when cutting conditions or overhang lengths change.
Every tool position presents a unique dynamic condition. As the gantry moves across the workpiece, changes in structural stiffness and mass distribution shift the machine’s natural frequencies, making high-performance machining a continuously moving target.
MAQ’s damped milling tools solve long-reach chatter directly at the source using Self-Tuning Mass Damper (STMD™) technology.
Key Advantages of MAQ STMD™ Damped Milling Tools:
- Automatic Frequency Adaptation: The internal damper dynamically adjusts its stiffness based on real-time vibration frequencies, providing optimal damping across varying overhang lengths and engagement conditions.
- Plug-and-Play Simplicity: MAQ damped milling tools require no electronic sensors, software dashboards, or manual operator tuning – simply clamp the holder and machine.
- Higher Productivity: Utilizing these advanced damped milling tools enables 30% to 50% higher feed rates and deeper axial cuts on long-reach shoulder, profile, and pocket operations.
- Superior Surface Quality and Tool Life: STMD™ technology in MAQ damped milling tools eliminates chatter marks to achieve fine Ra surface finishes while protecting brittle insert edges from impact chipping during heavy interrupted cuts.
By matching the right cutter geometry with MAQ’s self-tuning damped milling tools, shop floors can push the productivity limits of shoulder, profile, and pocket milling without sacrificing part quality. Explore MAQ’s complete line of damped milling tools to optimize your high-reach machining performance.